Capability: drawing, tooling, assembly and test under one roof
45,000 m² plant in Hebi, 1,500,000 harness and PDU sets per year. Engineering, cutting, crimping, assembly and electrical test are all in-house — we do not broker your order to a second factory.
Before we cut a wire, we agree on a drawing
Most harness quality problems are drawing problems that only appear at fitment. We front-load that risk.
Reverse engineering
Sample measured, every circuit mapped, connector families identified, wire gauge measured and cross-section checked. Output: a full 2D layout and circuit list.
3D routing & length verification
Where a vehicle is available or a scan is supplied, we verify branch lengths and routing before tooling. Branch length errors are the most common cause of a loom that will not reach.
Connector cross-reference
We maintain a library of Sumitomo, Yazaki, Aptiv, TE, Molex and KET footprints with terminal and seal part numbers, so an obsolete housing can be substituted with a documented equivalent instead of forced in.
Drawing package you keep
You receive the drawing, circuit list, connector list and test specification. It is your part number, not ours — you can second-source later without starting over.
Change control
Any revision after approval is versioned, and the test fixture is updated with it. No silent changes between batches.
DFM feedback
If a factory design has a weakness — a hinge loop without flex cable, a splice in a wet area — we flag it in the drawing review rather than reproduce the fault.
Equipment that matches the circuit count
| Cutting & crimping | Komax fully-automatic cut-strip-crimp lines for high-precision length, strip and crimp-height control; sealed-terminal and open-barrel applicators; pull force monitored per batch |
|---|---|
| Ultrasonic welding | SCHUNK ultrasonic wire splicers for multi-strand copper joints — no heat damage, lower resistance than a crimp splice; used on sensor, motor and HV shield terminations |
| Vision inspection | TSK inline camera systems checking crimp height, terminal seating and seal insertion on every piece, not a sample |
| Electrical test | TSK full-function test benches: continuity, insulation, dielectric strength and circuit resistance against the approved drawing; 100% of production, records ship with the cartons |
| Connector moulding | 20 imported FANUC precision moulding machines — connector housings and over-moulds are made in-house, so a broken tool never stops your order |
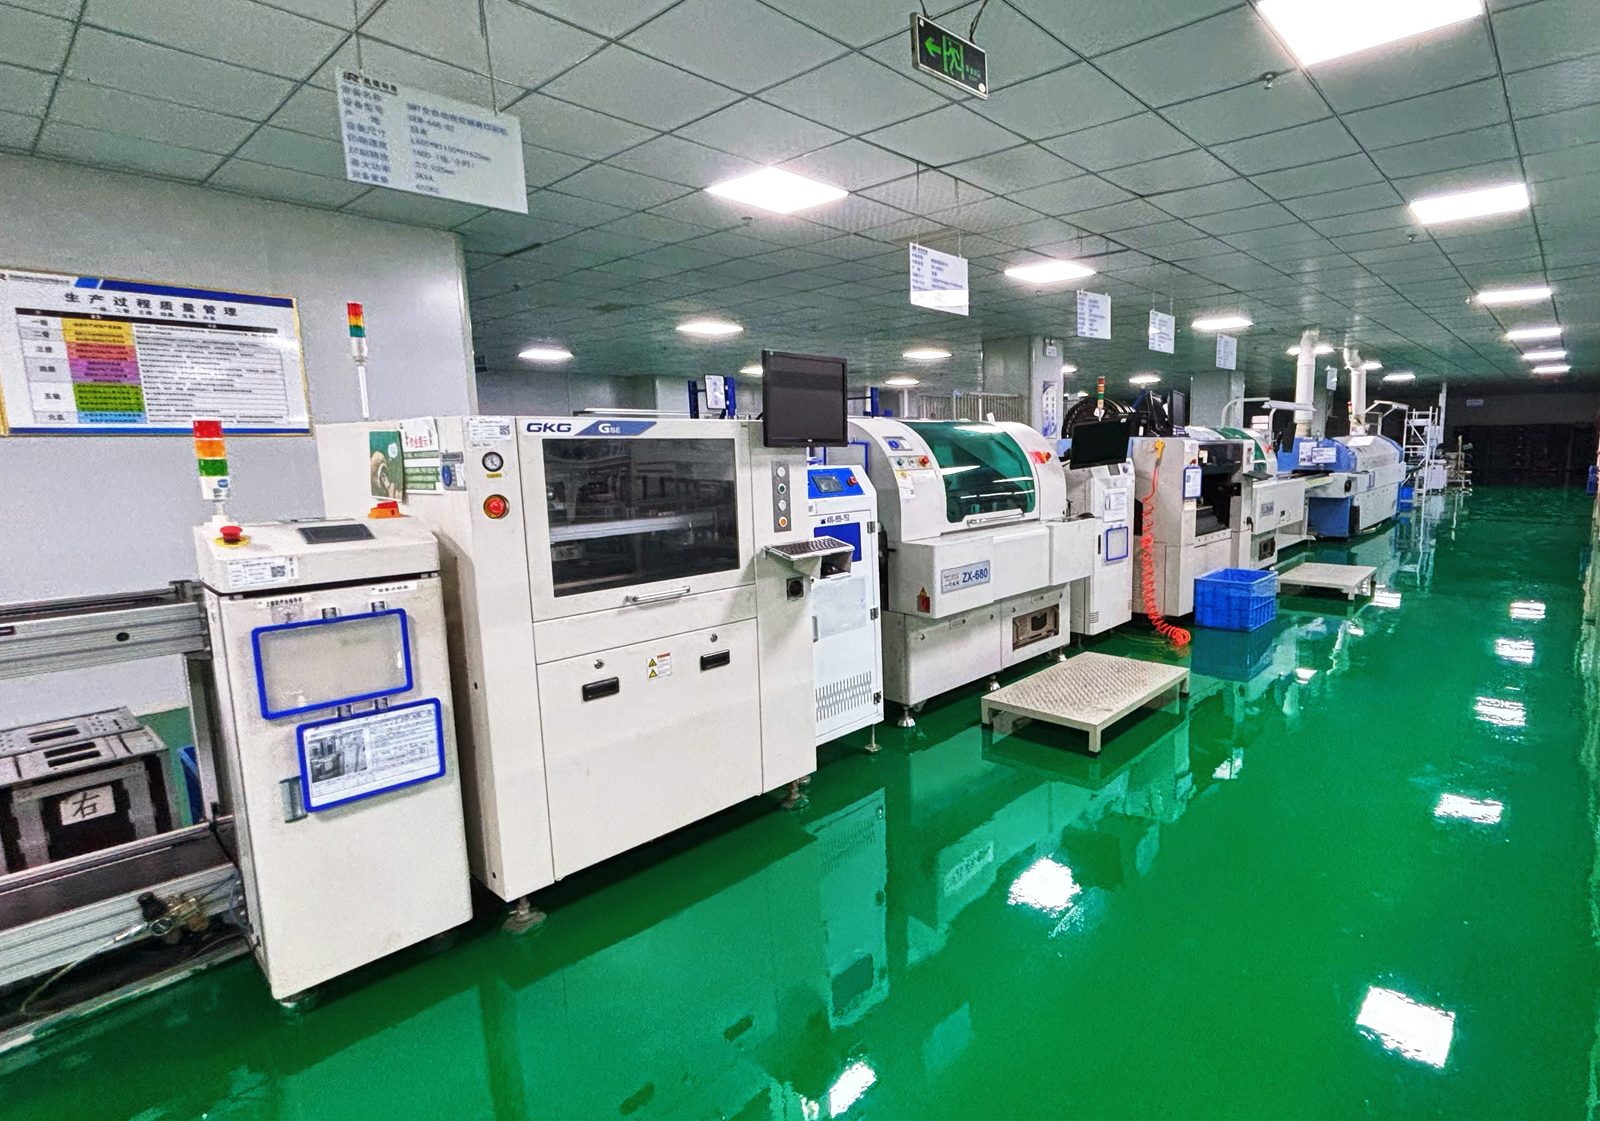
| Electronics | SMT lines and wave soldering for PDU and BDU control boards, assembled and tested in the same plant as the harness they plug into |
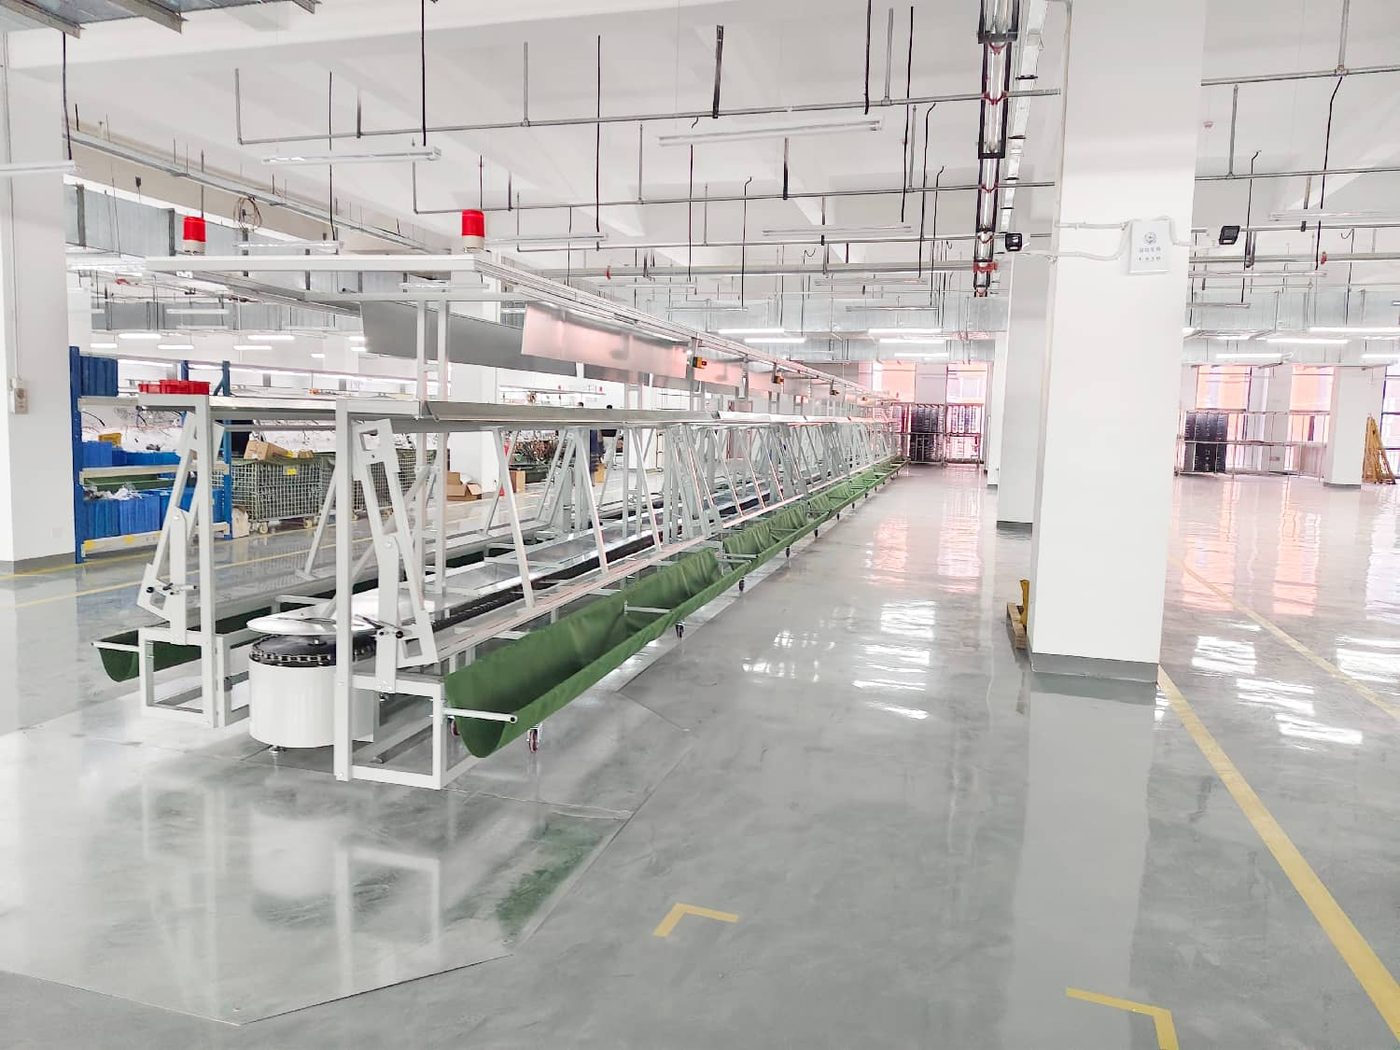
| Workshops | 45,000 m² across four specialised units: SMT, connector moulding, PDU automation and HV / low-voltage harness assembly |
| Capacity | 1,500,000 HV harness and PDU sets per year on current lines; a dedicated 300,000-set-per-year full-vehicle harness plant comes on stream in H2 2026 |
Specified, not substituted
Wire
TXL (irradiated PVC, 125 °C), GXL (glass braid), TPE for flex sections and silicone for high-temperature branches. Copper is sourced with a mill certificate per lot.
Connectors & terminals
Original series from Sumitomo, Yazaki, Aptiv, TE, Molex, KET or a documented equivalent agreed with you in writing before production.
Protection
PVC and non-woven tape, corrugated and split conduit, heat-shrink breakouts, grommets and sealed pass-throughs selected for the environment the branch actually sees.
HV materials
Shielded 600/800 V cable, orange jacket, HVIL terminals and IP67 connectors, with hipot and insulation-resistance test on every assembly.
The numbers buyers ask for first
Need a different structure — consignment stock, Kanban release, or a frame agreement with annual pricing? Ask; those are normal for fleet and distributor accounts.
Send the drawing. Get a quote and a sample date inside 24 hours.
Email a photo of the OEM label, a pin-out or the old loom itself. Our engineers will confirm fitment, circuit count and connector family, then send a quote and a sample date within 24 hours. Samples ship in 7–10 days; production takes 25–30 days.